Through machining, welding and straightening, vacuum parts pick up coolant, hand oils, heat tint and chips. At atmospheric pressure none of it shows; under vacuum it becomes an outgassing and particle source — longer pump-down, unreachable ultimate vacuum, pinholes in coating. Cleaning and packing are part of the process, not a wipe before dispatch.
1. Cleaning sequence
- Deburr — scraper, stone and deburring tool; cross-holes and thread entries first.
- Pre-clean — alkaline cleaner or ultrasonic bath to remove coolant and oil.
- Rinse — deionised or purified water, so tap-water minerals are not left behind.
- Dry — compressed air plus oven drying; blow out threaded and blind holes separately.
- Wipe — lint-free cloth with IPA on sealing and mating faces until the cloth comes away clean.
- Protect — pickle and passivate stainless parts as required to remove weld tint and restore the passive layer.
2. Packing
- Protective rings or soft pads on sealing faces and knife edges; no bare metal-to-metal contact.
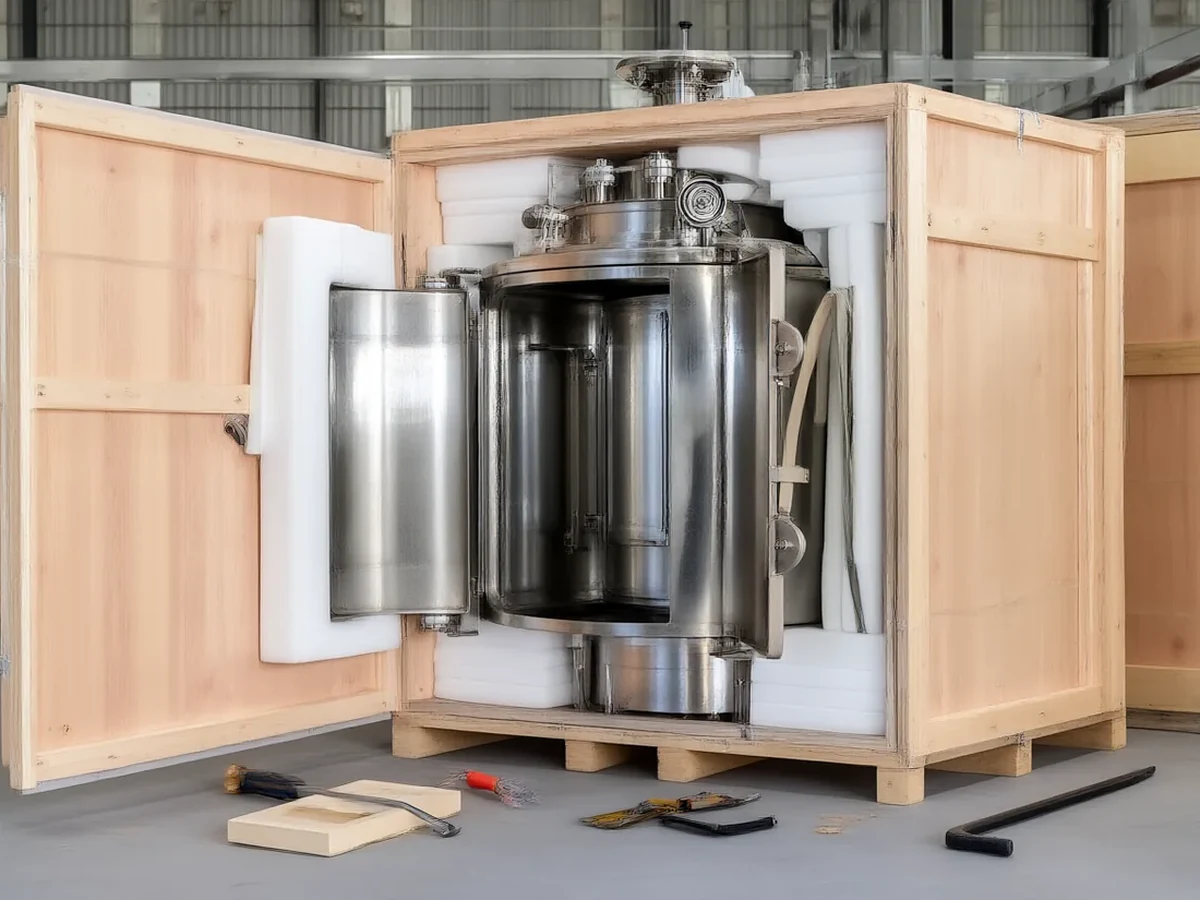
- Inner foil or vacuum bag with desiccant; outer crate or reinforced carton.
- Humidity indicator card inside; vacuum-then-nitrogen fill for long sea freight.
- Mark cartons "precision parts — no impact"; flanges fixed separately, never mixed with heavy items.
3. Five-point incoming inspection
- Packing integrity: bag intact, indicator card still indicating dry.
- Visual: sealing faces, knife edges and thread entries free of knocks, rust or loose particles.
- White-cloth wipe: no visible stain on mating faces.
- Dimensional spot check: key sealing dimensions and hole positions.
- Pre-assembly clean: IPA wipe at the assembly bench, gloves on.
Our default delivery standard for vacuum parts: deburred, degreased, DI-water rinsed, dried, sealing faces wiped, protection rings + foil bag + desiccant. State passivation, electropolishing or particle counting on the inquiry if required.